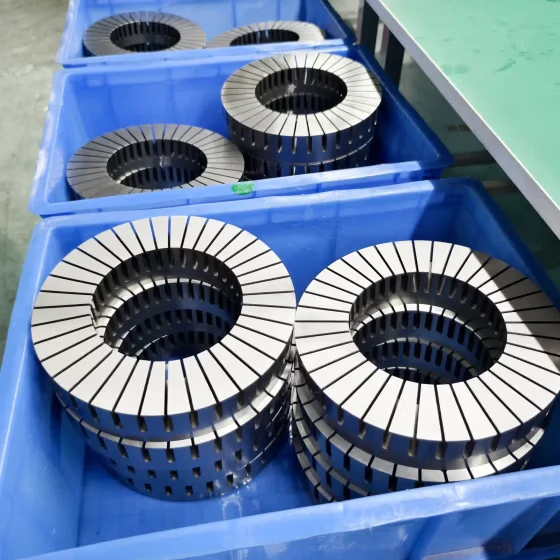
brushless motor
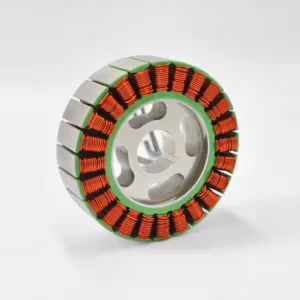
Production process of stator iron core for axial flux motor
Axial Flux Motor Stator Iron Core Production Process
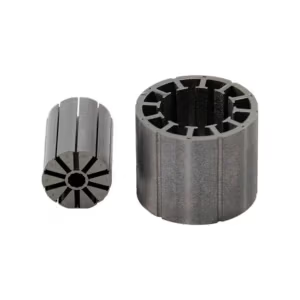
Axial flux motors attract strong interest in electric vehicles, robotics, and high-efficiency industrial drives. As a result, manufacturers now pay closer attention to the motor stator Iron Core, which directly affects efficiency and torque output.
In this article, we explain the production process of an axial flux stator core step by step. By doing so, engineers and B2B buyers can understand how core quality influences motor performance and long-term reliability.
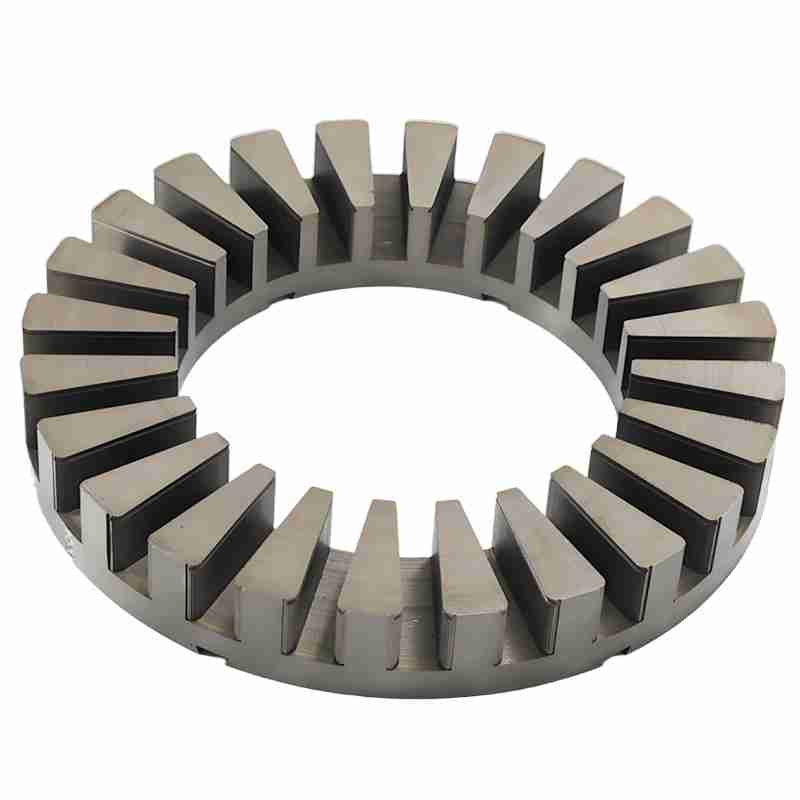
Why the Stator Core Matters
The stator iron core guides magnetic flux through the motor. Therefore, its structure and material quality strongly influence efficiency, torque density, and heat generation.
More importantly, axial flux motors operate with a very small air gap. Because of this, even small deviations in the stator core can reduce overall motor performance.
Step 1: Electrical Steel Selection
The production process starts with electrical steel selection for the motor stator core. In most designs, manufacturers choose non-oriented silicon steel.
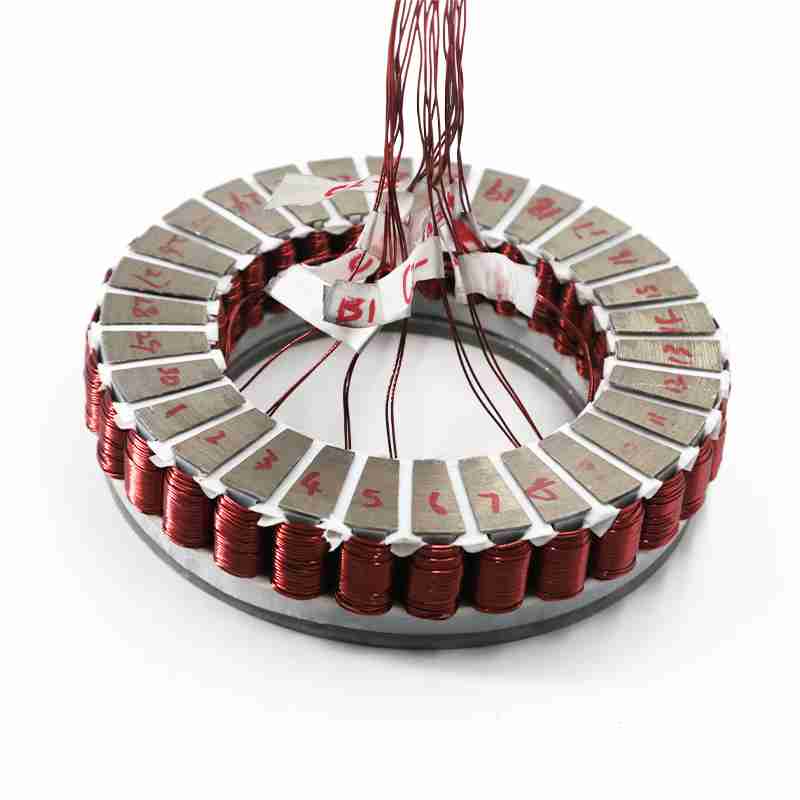
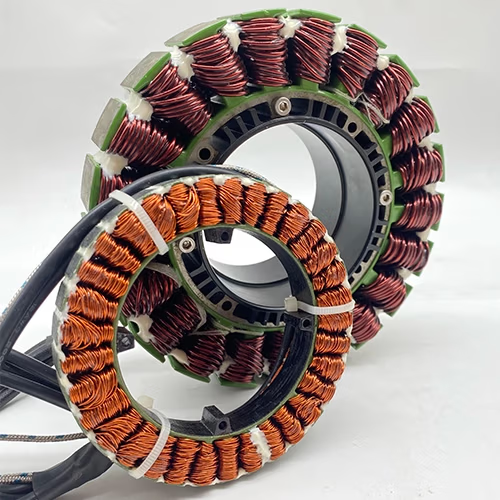
Process of stator winding for axial flux motor
Engineers prefer this material because it provides:
-
Low iron loss in the stator core
-
Stable magnetic behavior
-
Good mechanical strength
In addition, many projects use thin laminations between 0.2 mm and 0.35 mm. As a result, the stator iron core delivers higher efficiency and lower eddy current loss.
Step 2: Stator Lamination Design
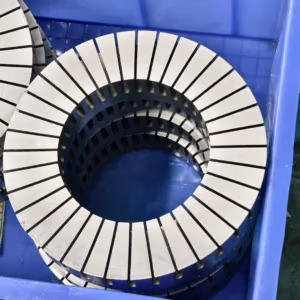
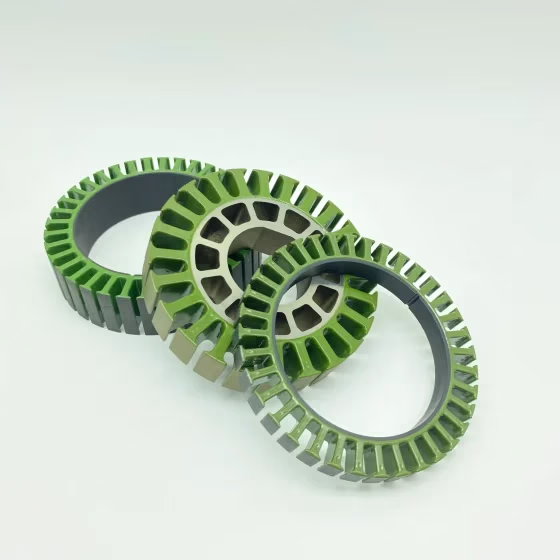
Next, engineers focus on stator lamination design, which defines the shape of the axial flux stator core. Unlike radial motors, axial flux motors rely on flat, disc-shaped laminations.
Typically, designers include:
-
Disc or segmented laminations
-
Concentrated tooth structures
-
Optimized slot geometry
Because of this layout, the stator core achieves higher copper fill and smoother torque output.
Step 3: Lamination Cutting Process
After finalizing the design, the production team cuts laminations for the stator core. At this stage, two cutting methods dominate the process.
High-Speed Stamping
Manufacturers use stamping for large-scale stator core manufacturing. For this reason, it offers high consistency and low unit cost.
Laser Cutting
Teams use laser cutting during prototyping. Although the speed is lower, this method allows fast design changes without tooling.
In both cases, operators carefully control burr height and flatness to protect magnetic performance.
Step 4: Insulation Coating
After cutting, operators apply an insulation coating to each lamination. This step matters, because it limits eddy current loss inside the core stack.
Most manufacturers use C5 or C6 inorganic coatings. Meanwhile, designers select organic coatings when higher slot fill is required.
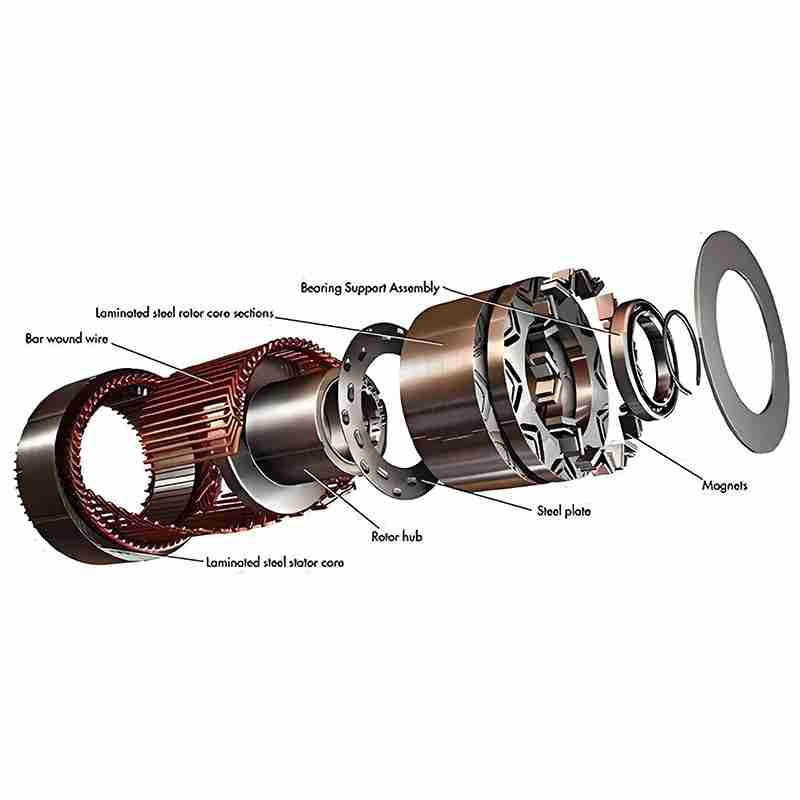
Step 5: Stator Core Stacking and Assembly
Once coating is complete, workers stack laminations to form the stator assembly. Depending on the motor design, manufacturers select different core structures.
For example:
-
Full disc stator cores provide high rigidity
-
Segmented stator designs simplify winding
As a result, segmented axial flux stator cores are widely used in modern motors.
Step 6: Compression and Annealing
After stacking, the team applies axial compression to the stator assembly. This step ensures tight contact between laminations.
In addition, manufacturers often perform stress relief annealing. By restoring magnetic properties, annealing reduces iron loss and improves efficiency.
Step 7: Precision Machining
Axial flux motors react strongly to air gap changes. Therefore, manufacturers perform precision machining with strict control.
Technicians grind the core surface and machine inner and outer diameters. At the same time, they prepare mounting features to ensure accurate motor assembly.
Step 8: Impregnation and Surface Protection
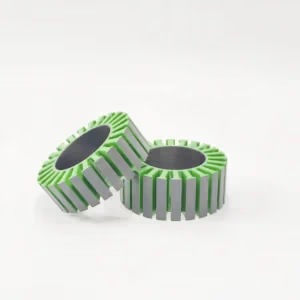
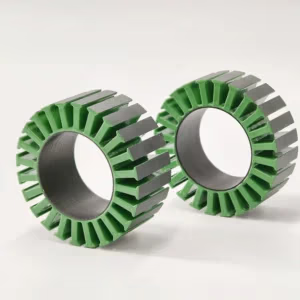
For demanding applications, manufacturers add extra protection. For instance, they use vacuum pressure impregnation or epoxy coating.
As a result, the stator structure gains higher mechanical strength, better vibration resistance, and improved heat transfer.
Step 9: Quality Inspection
Before delivery, inspectors test each stator assembly. At this point, they check dimensions, flatness, and magnetic performance.
Only after passing inspection does the component move to final motor assembly.
Stator Core Production Flow
Electrical Steel → Lamination Cutting → Insulation → Stacking → Compression → Annealing → Machining → Inspection
Final Thoughts
In summary, a well-controlled stator core manufacturing process supports high efficiency and compact motor design. Not only does high core quality improve torque density, but it also enhances long-term reliability.
As axial flux motors continue to grow, advanced stator core manufacturing will remain a key competitive advantage.